Visão geral
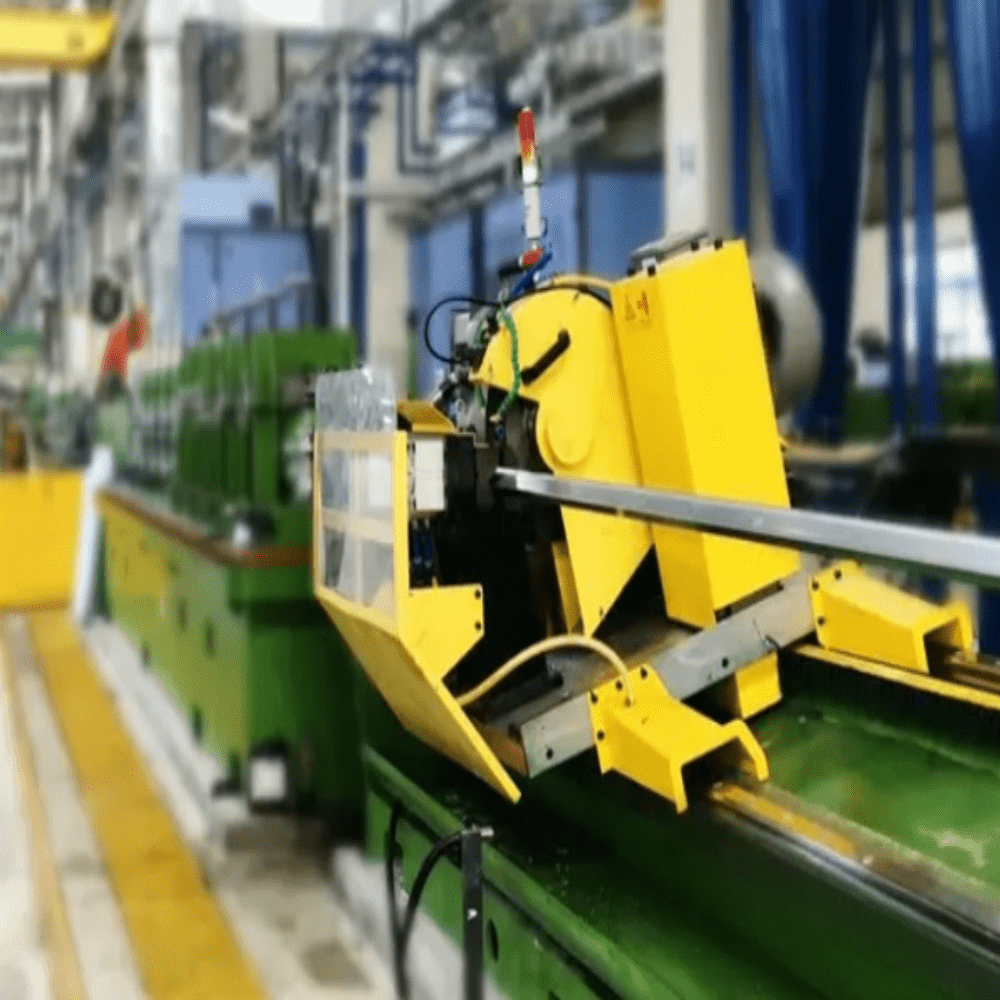
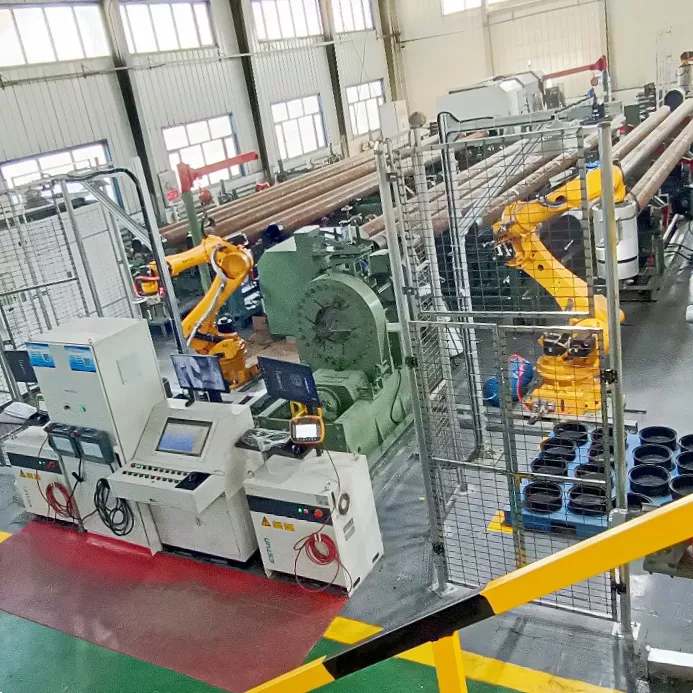
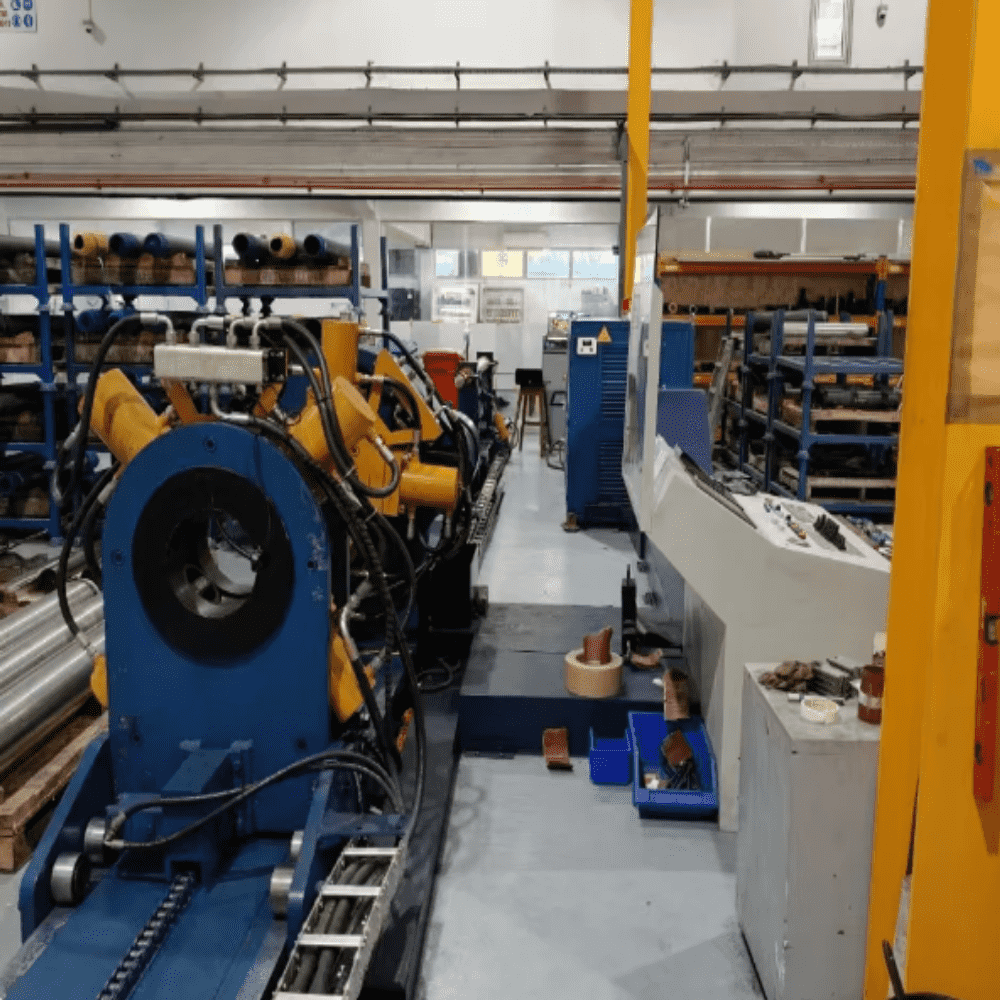
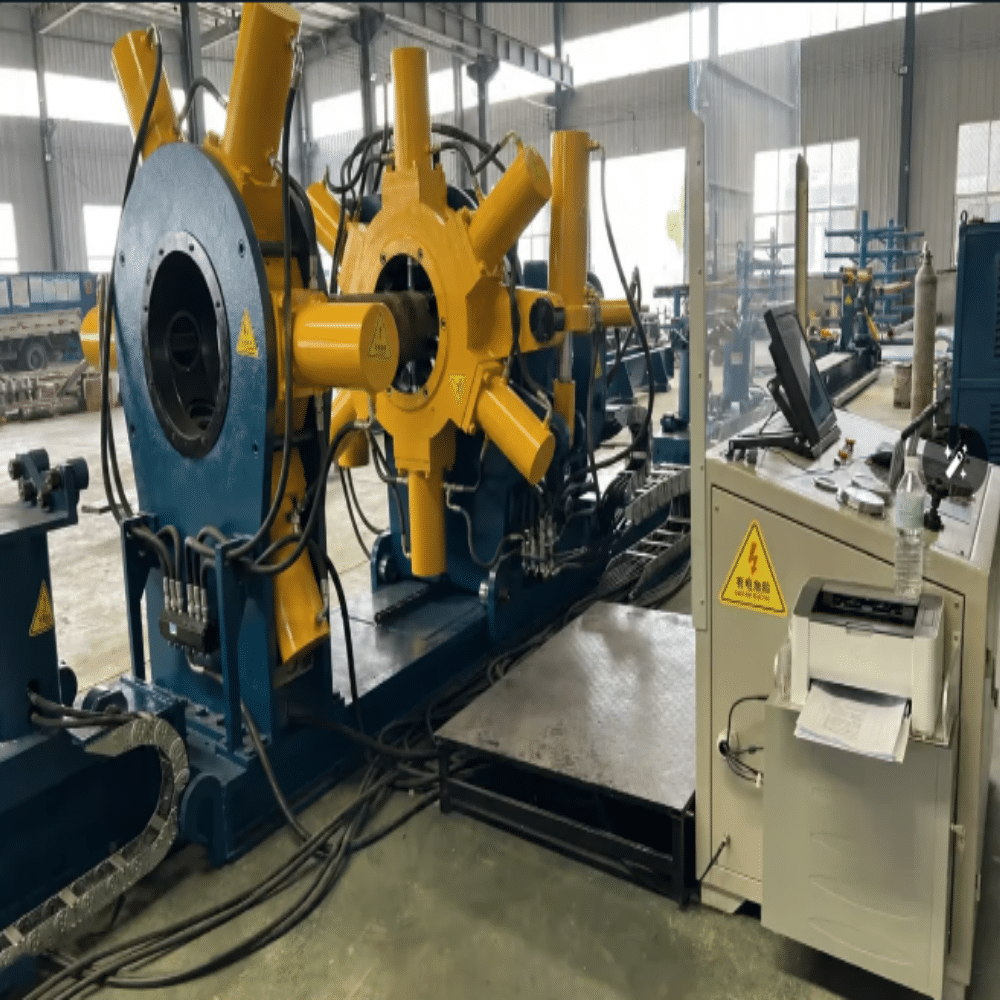
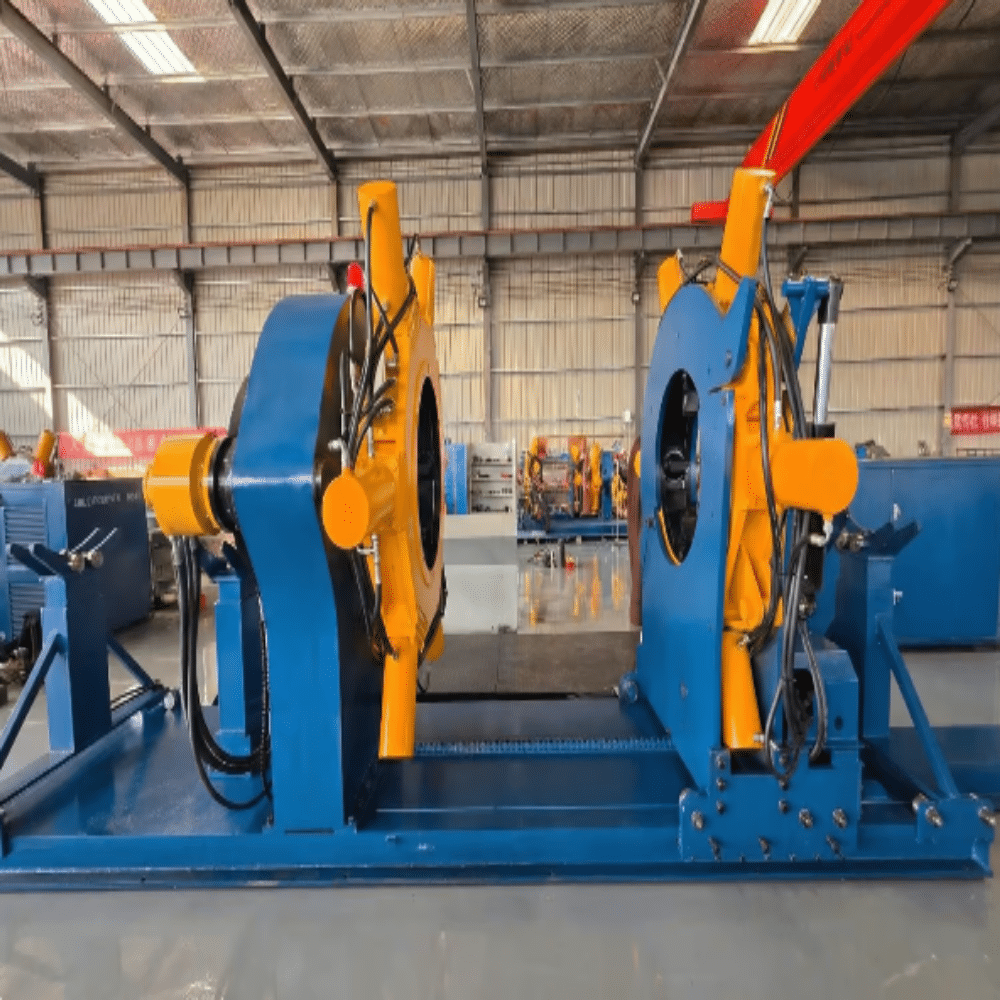
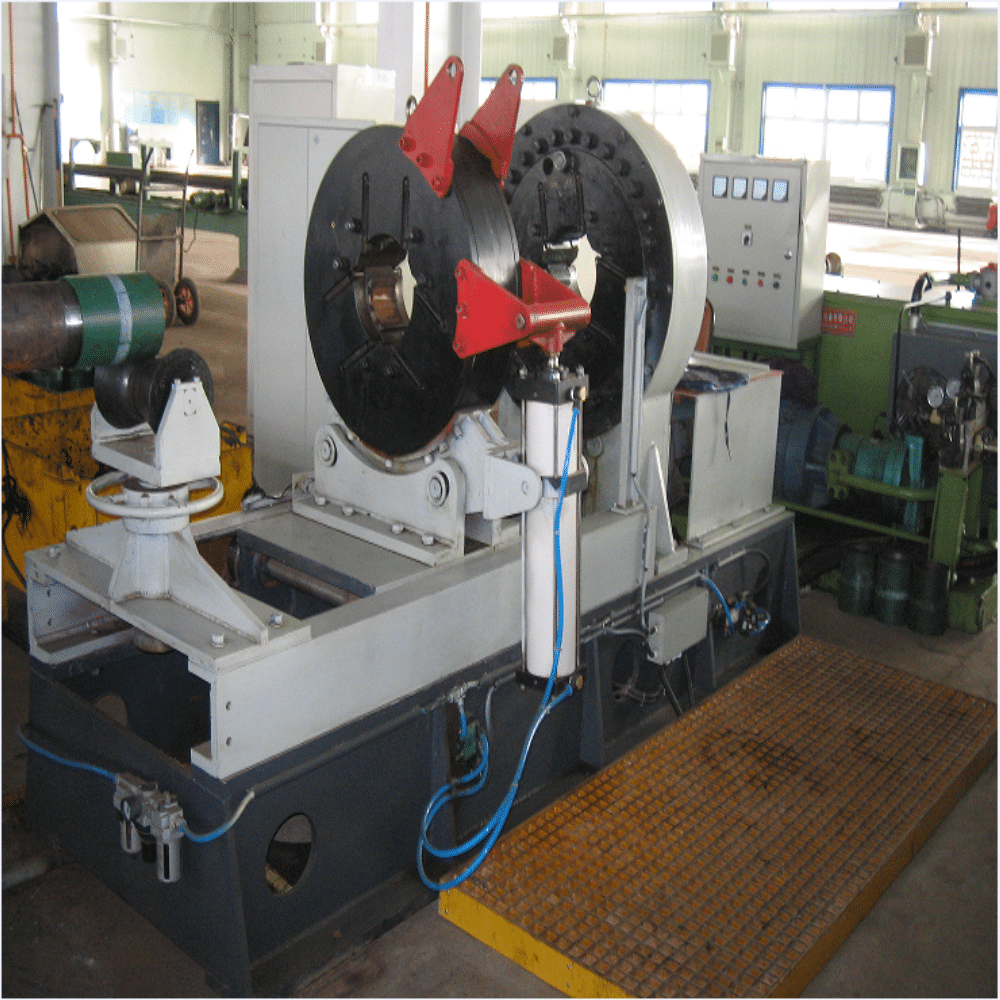
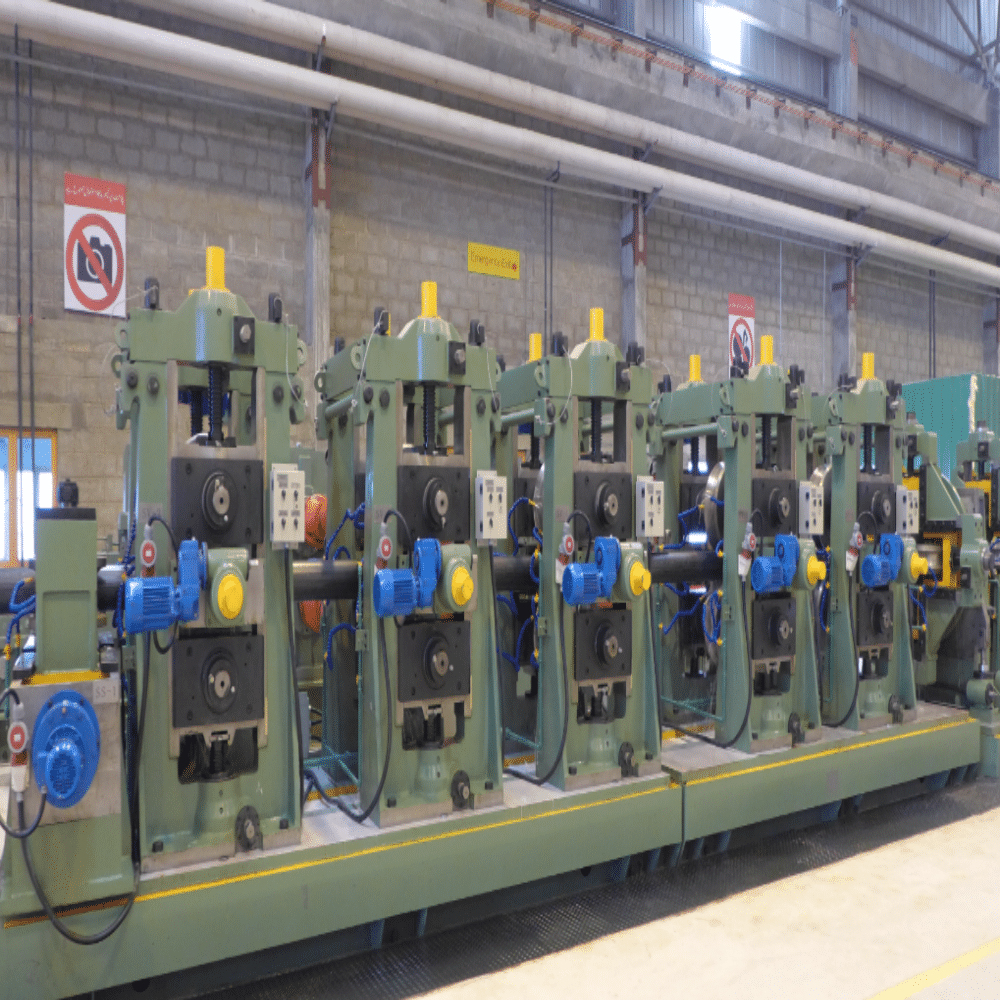
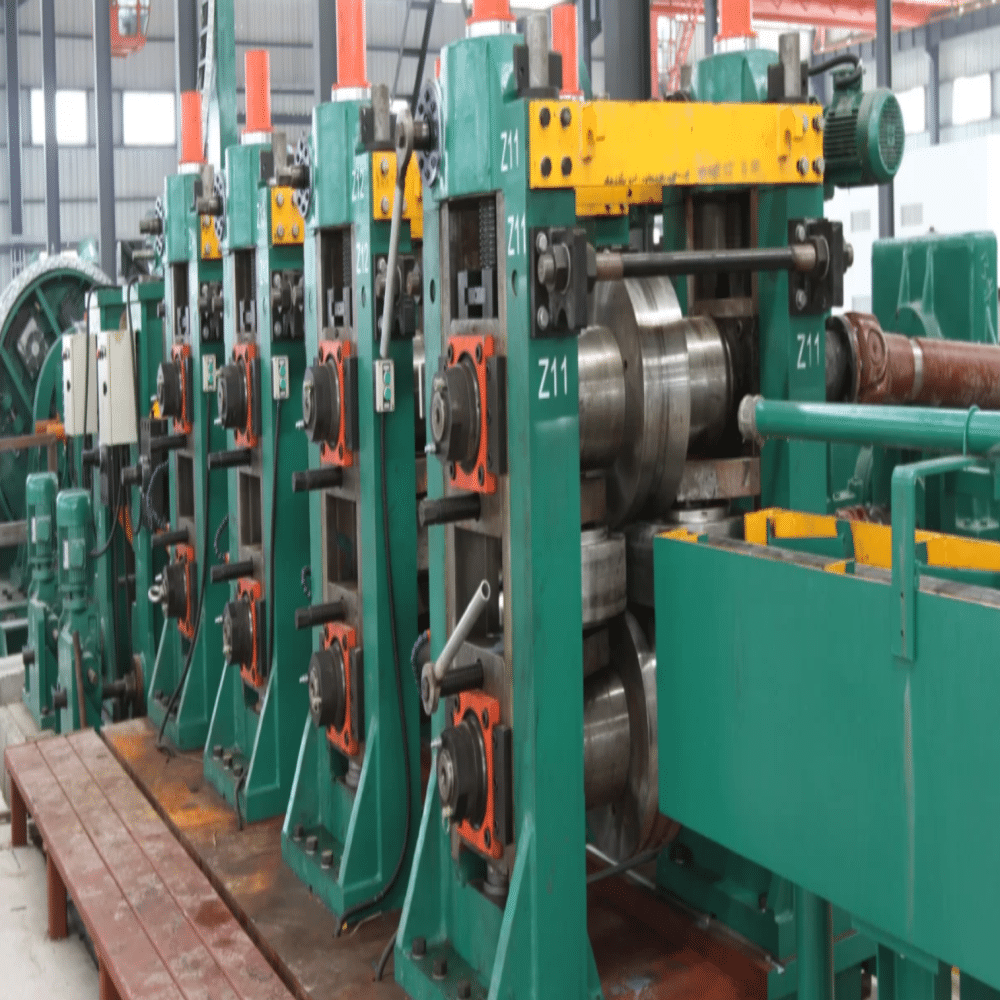
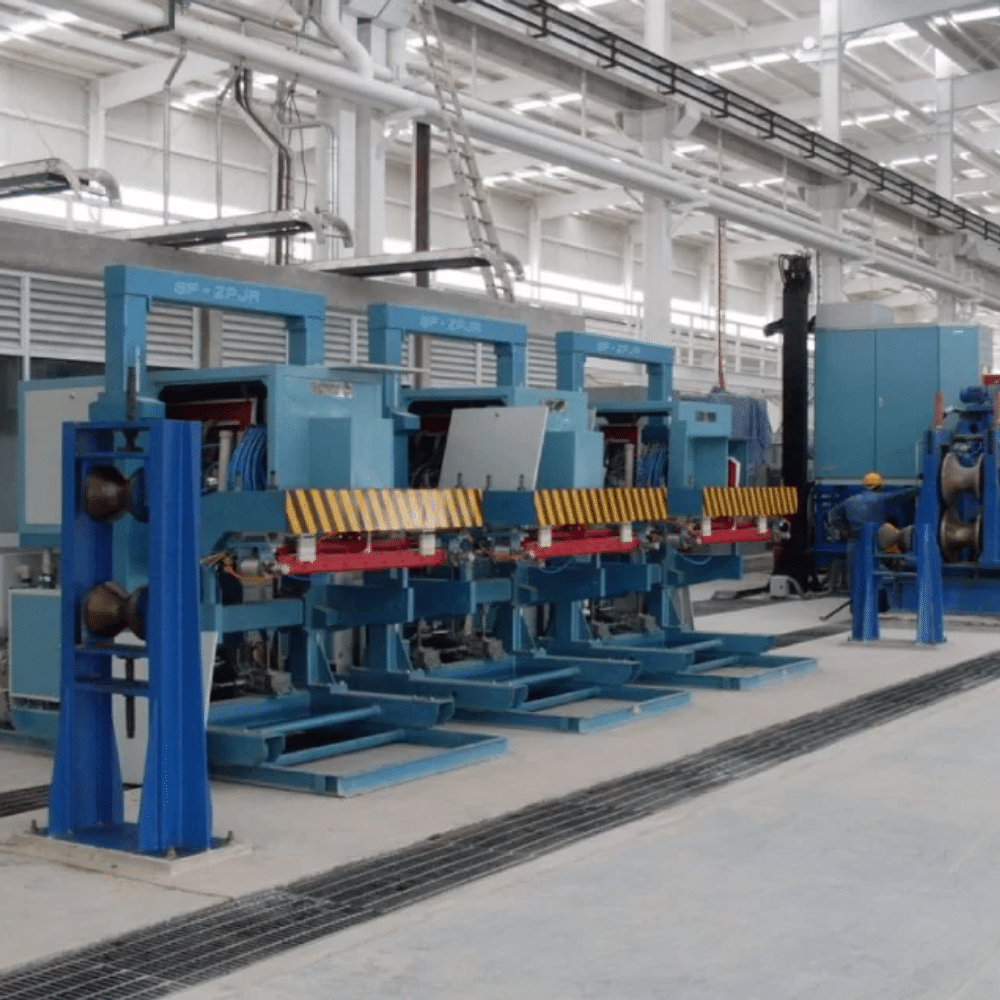
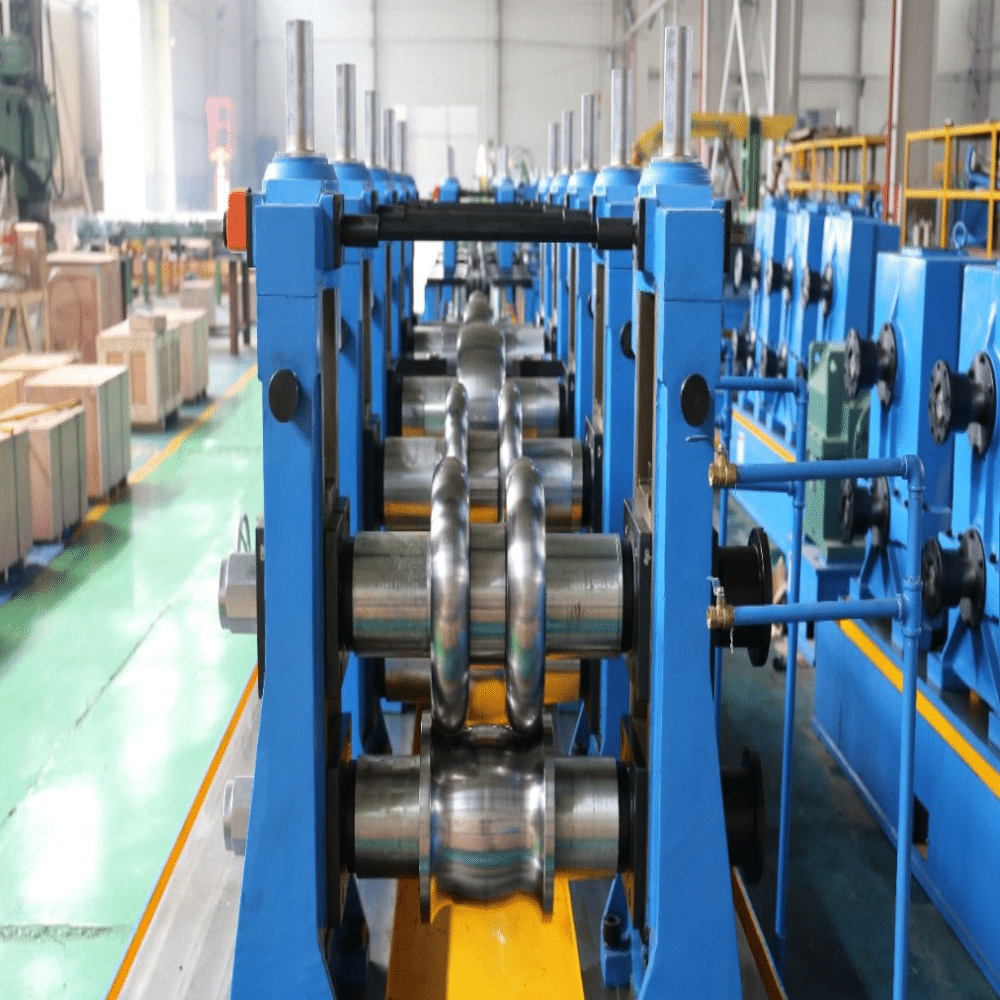
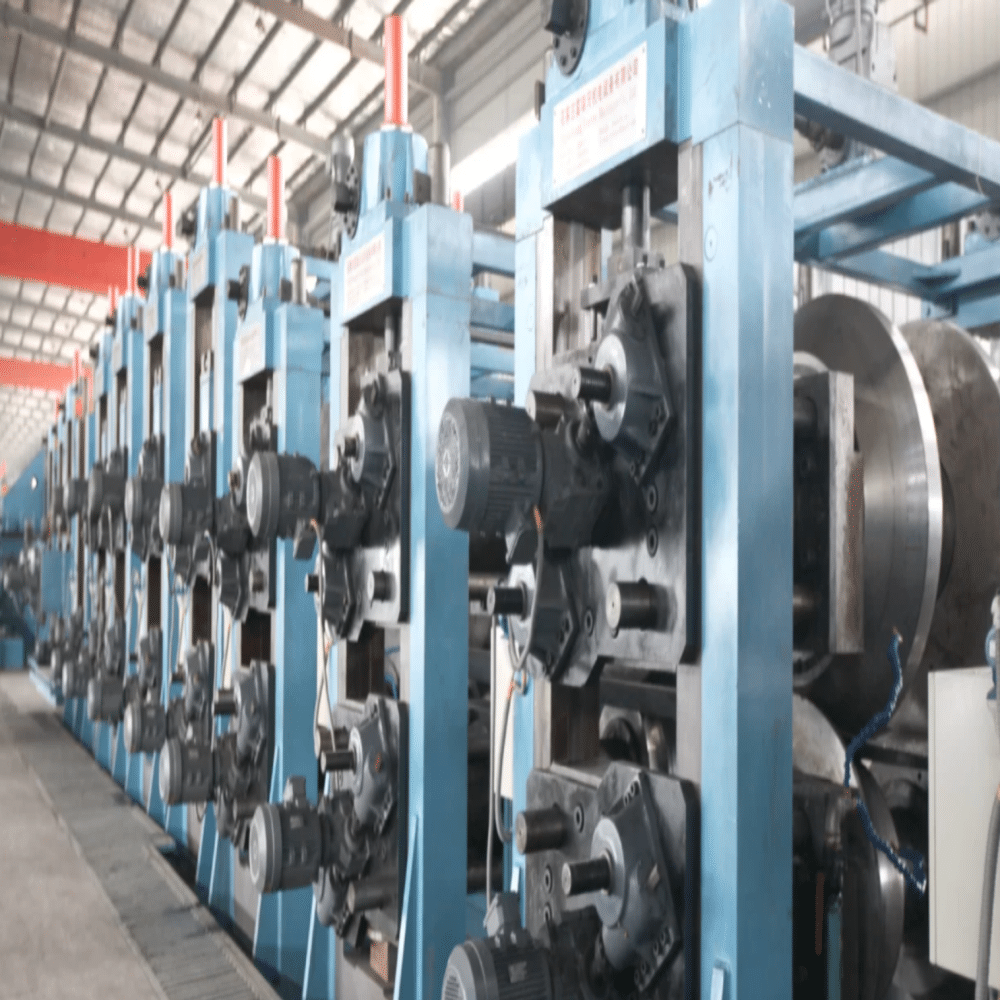
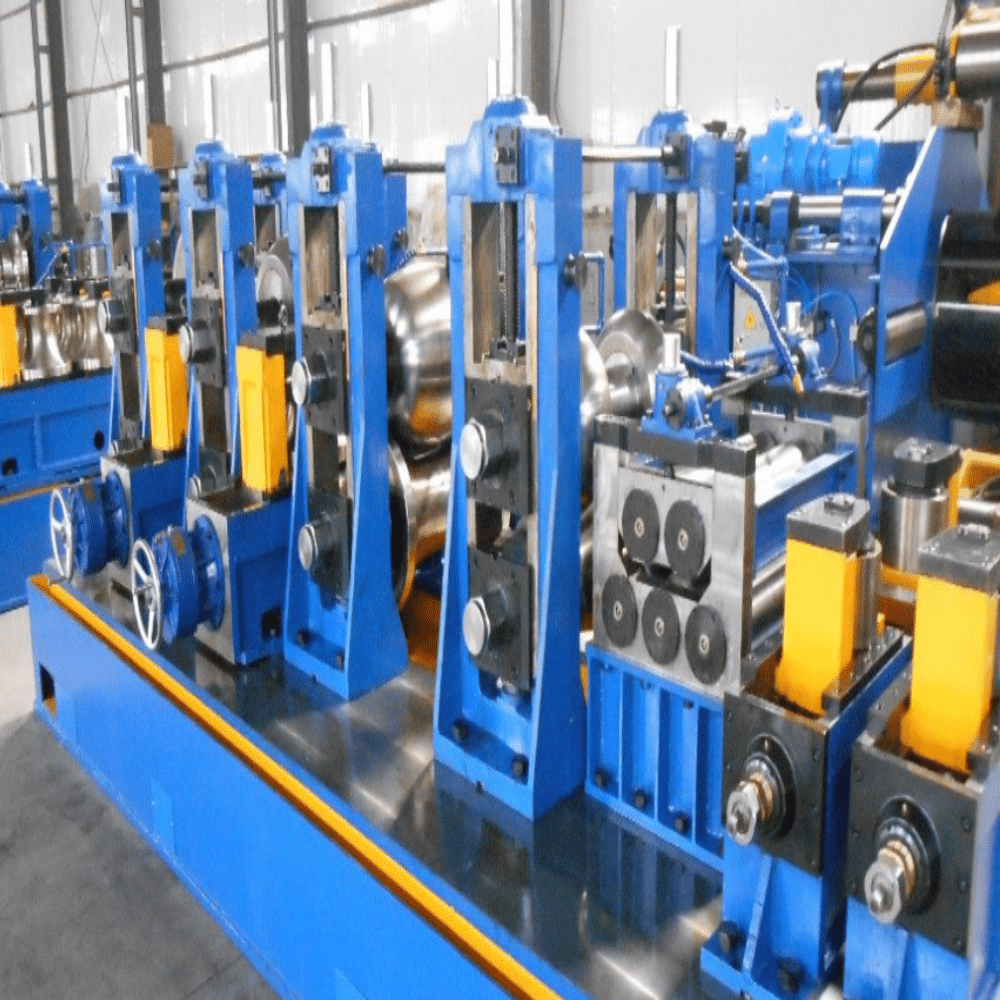
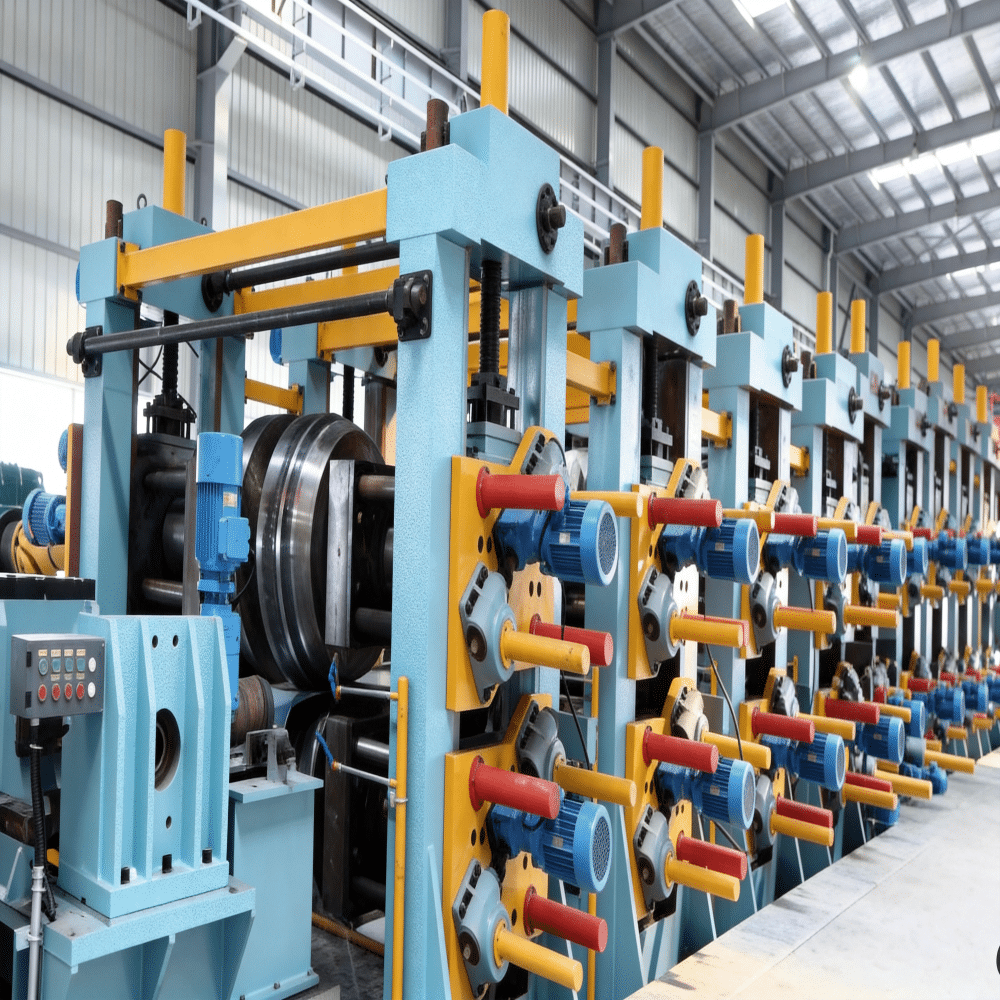
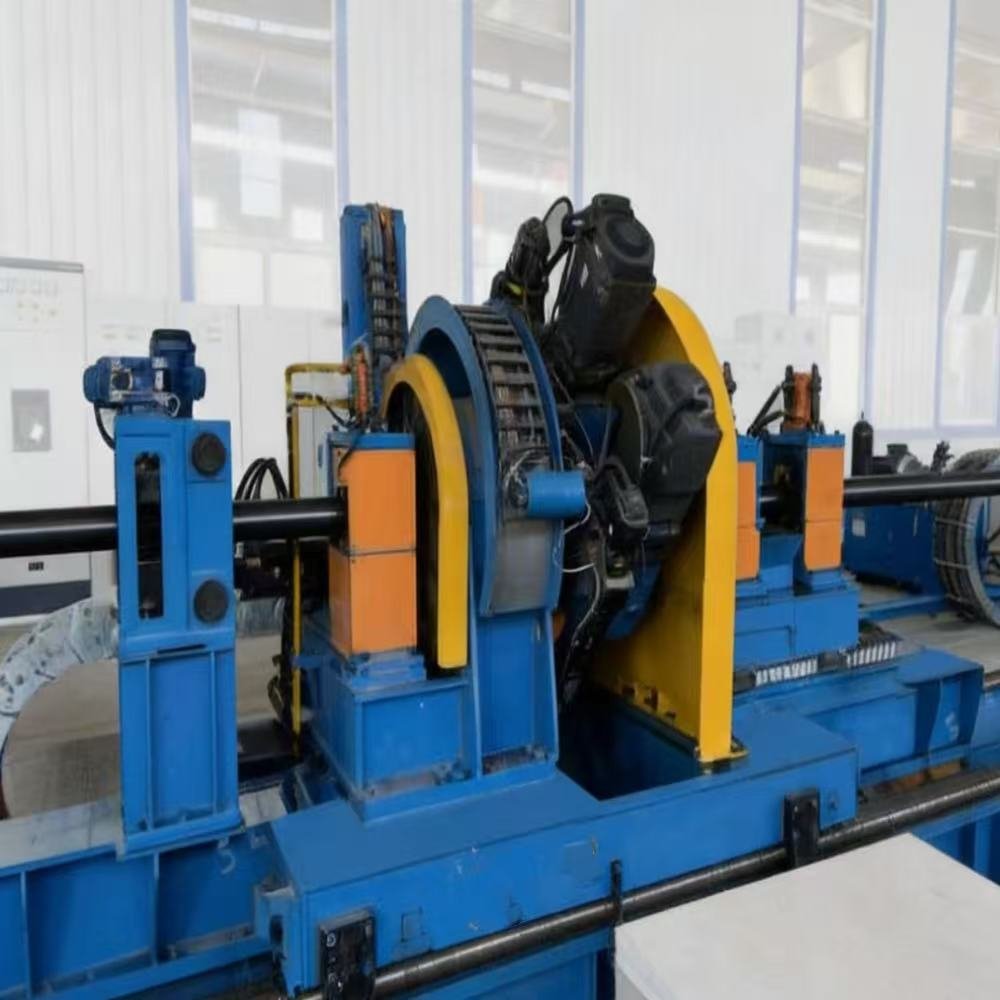
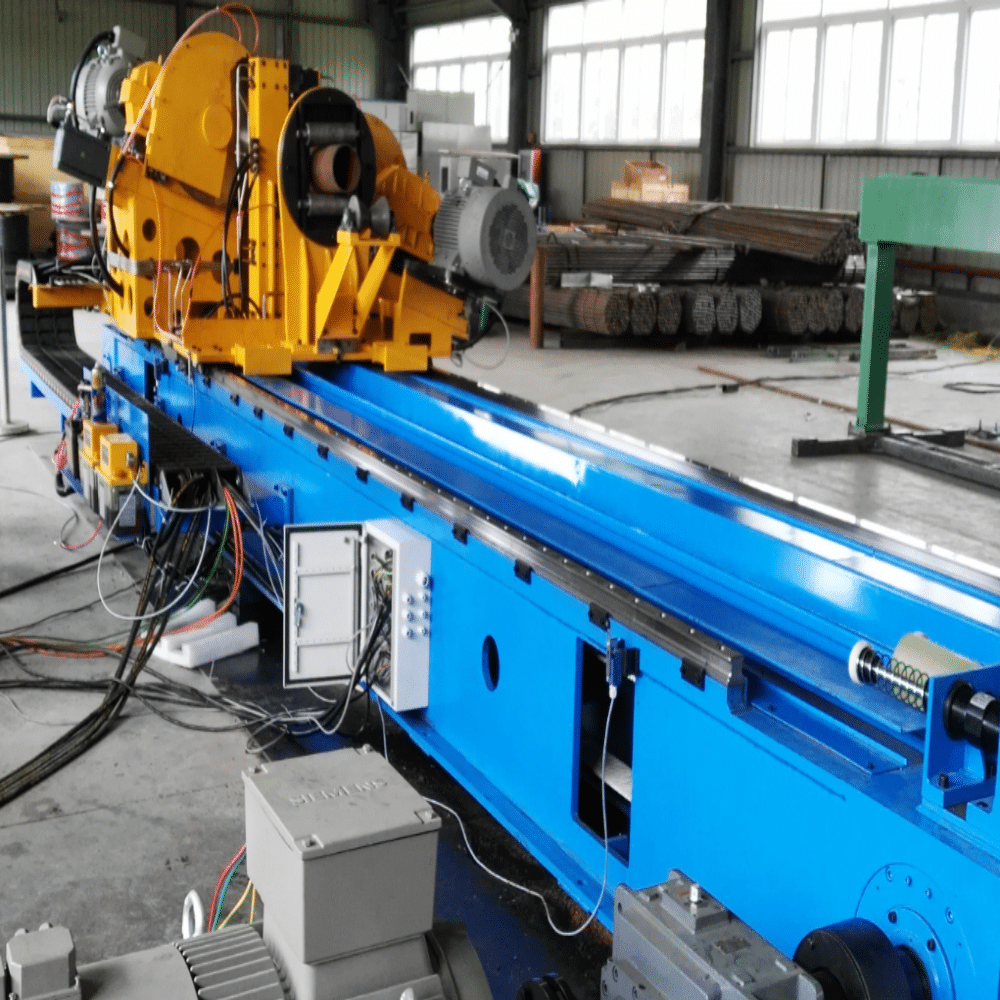
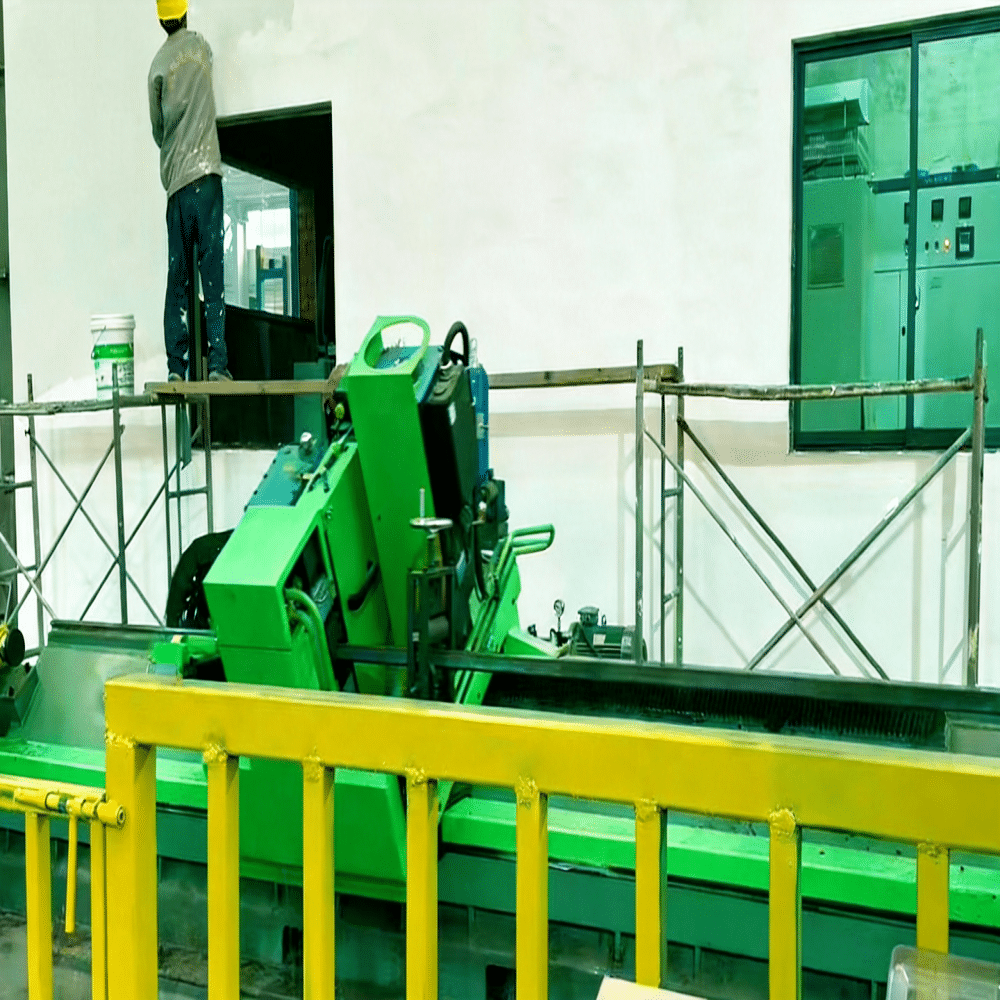
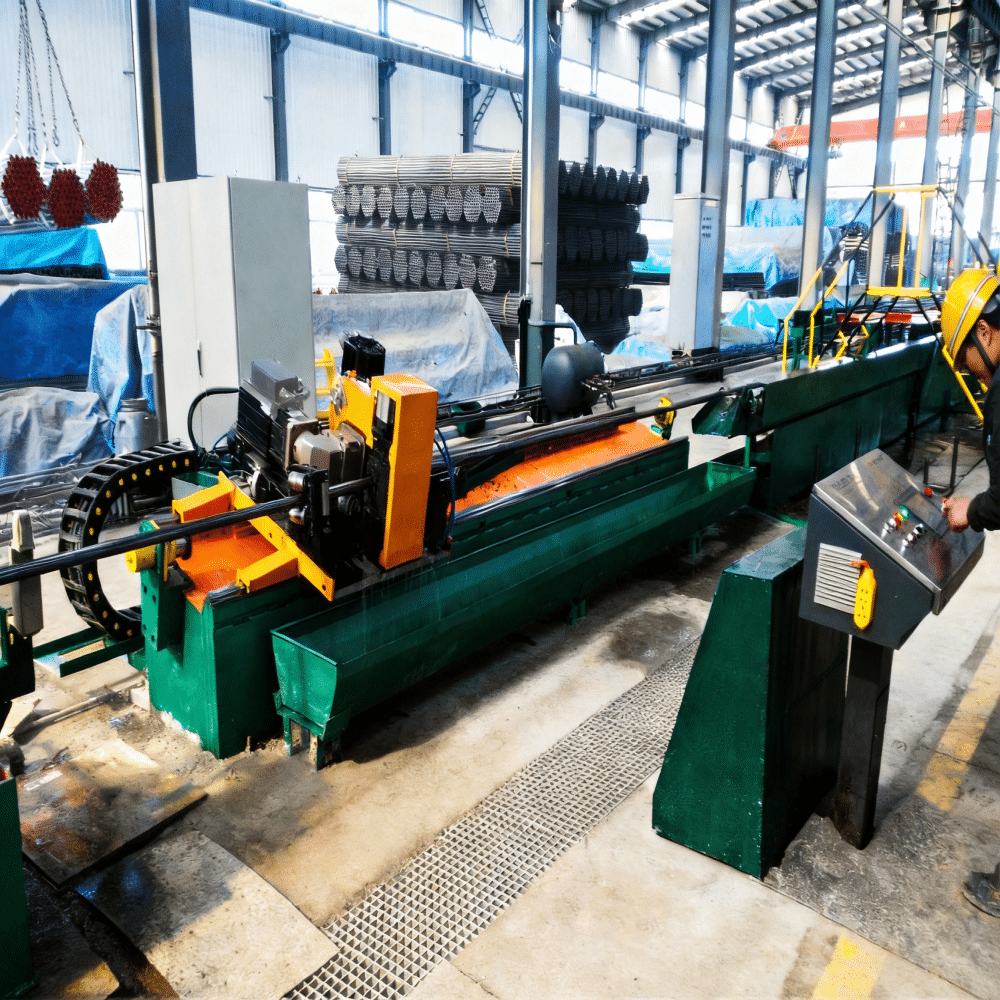
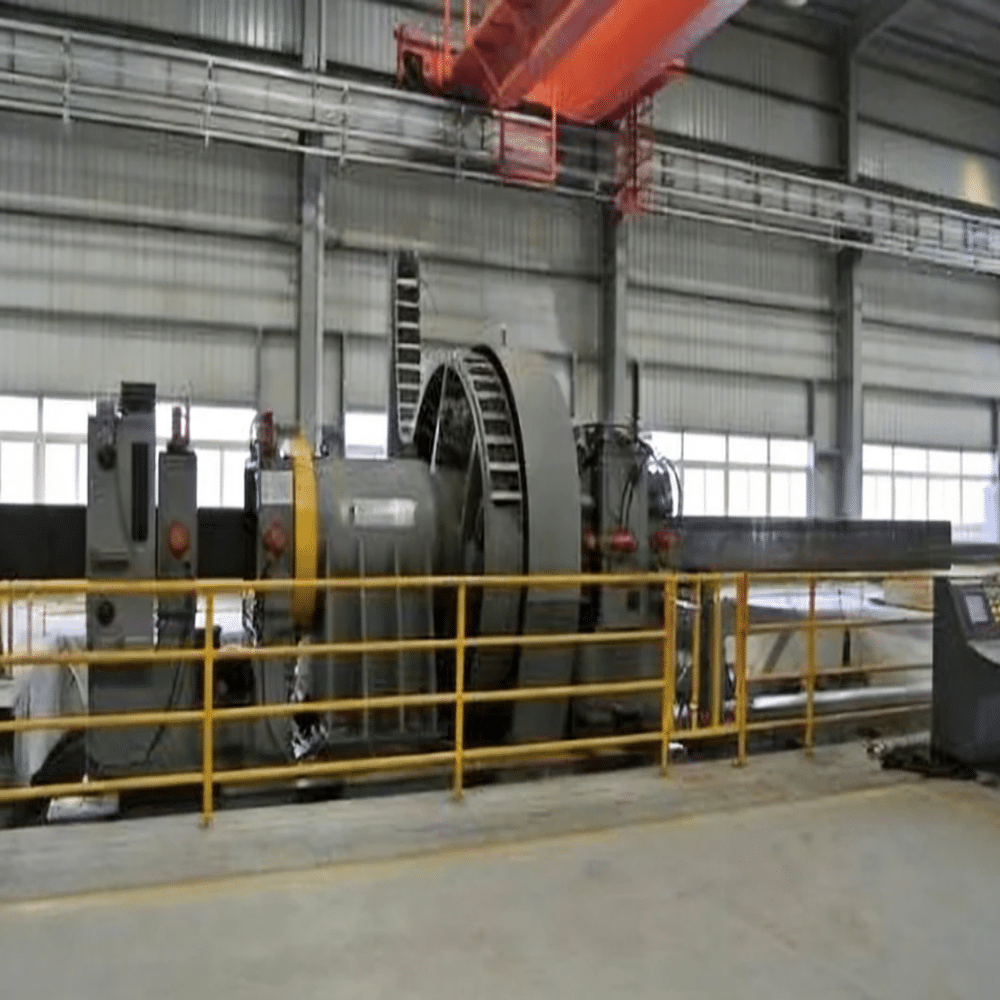
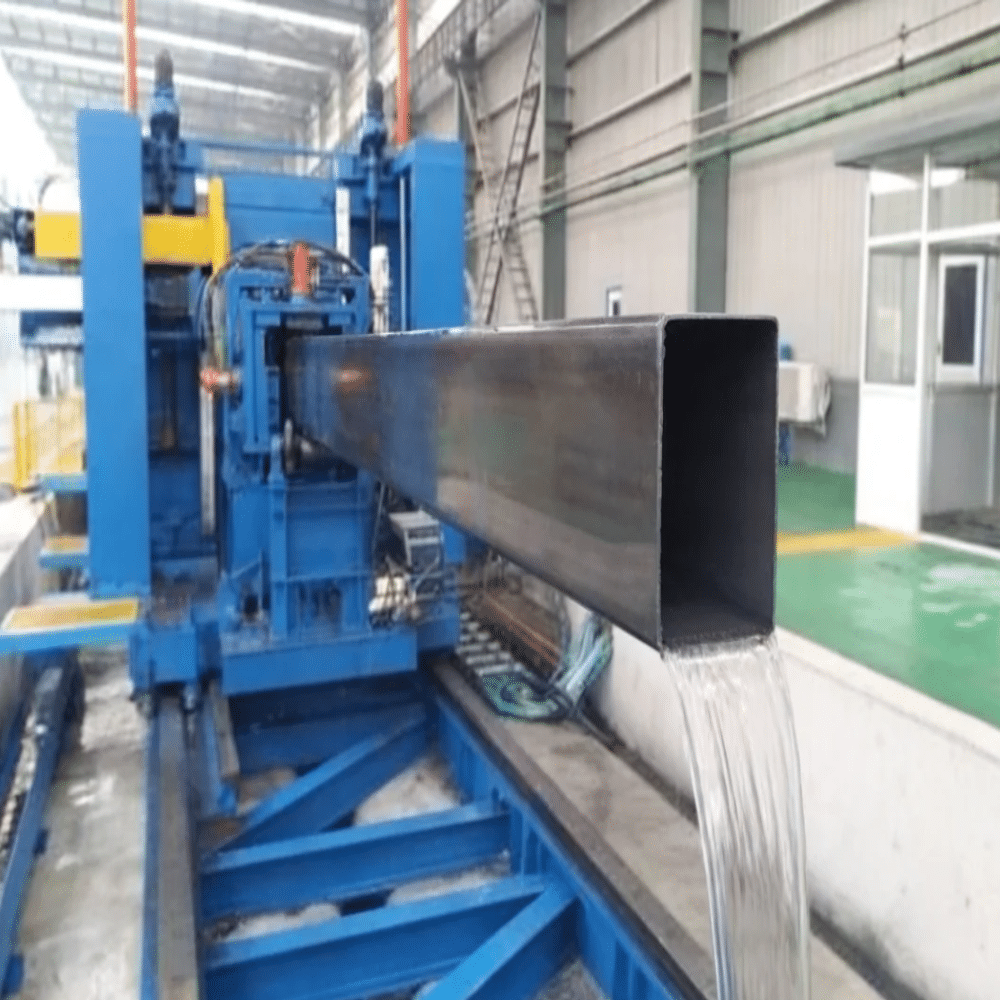
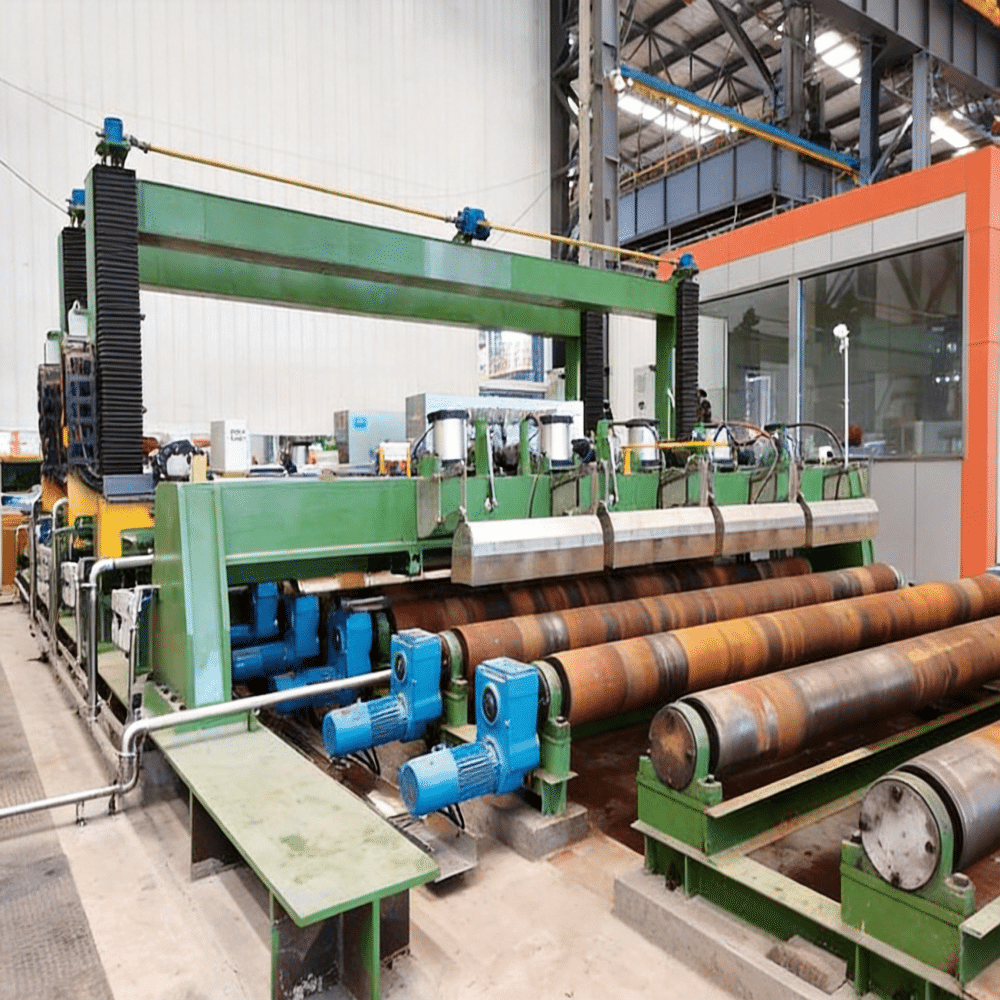
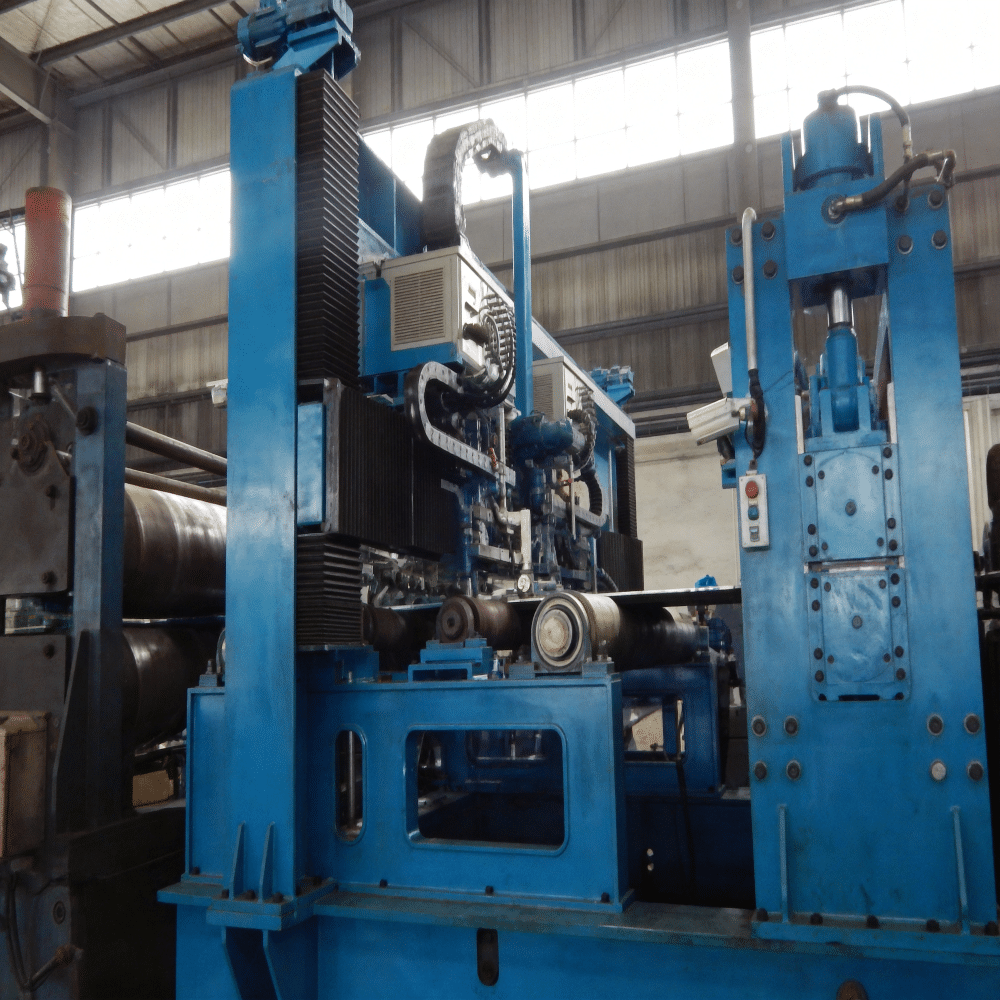
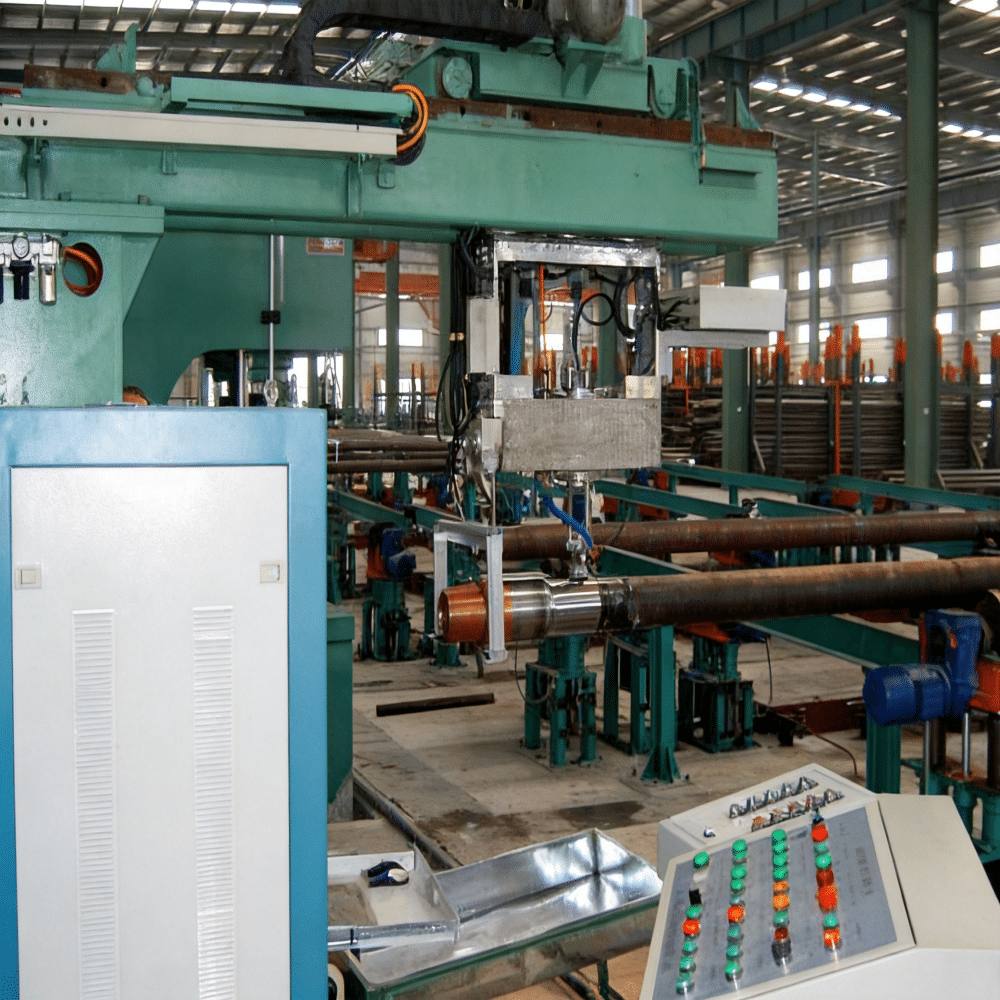
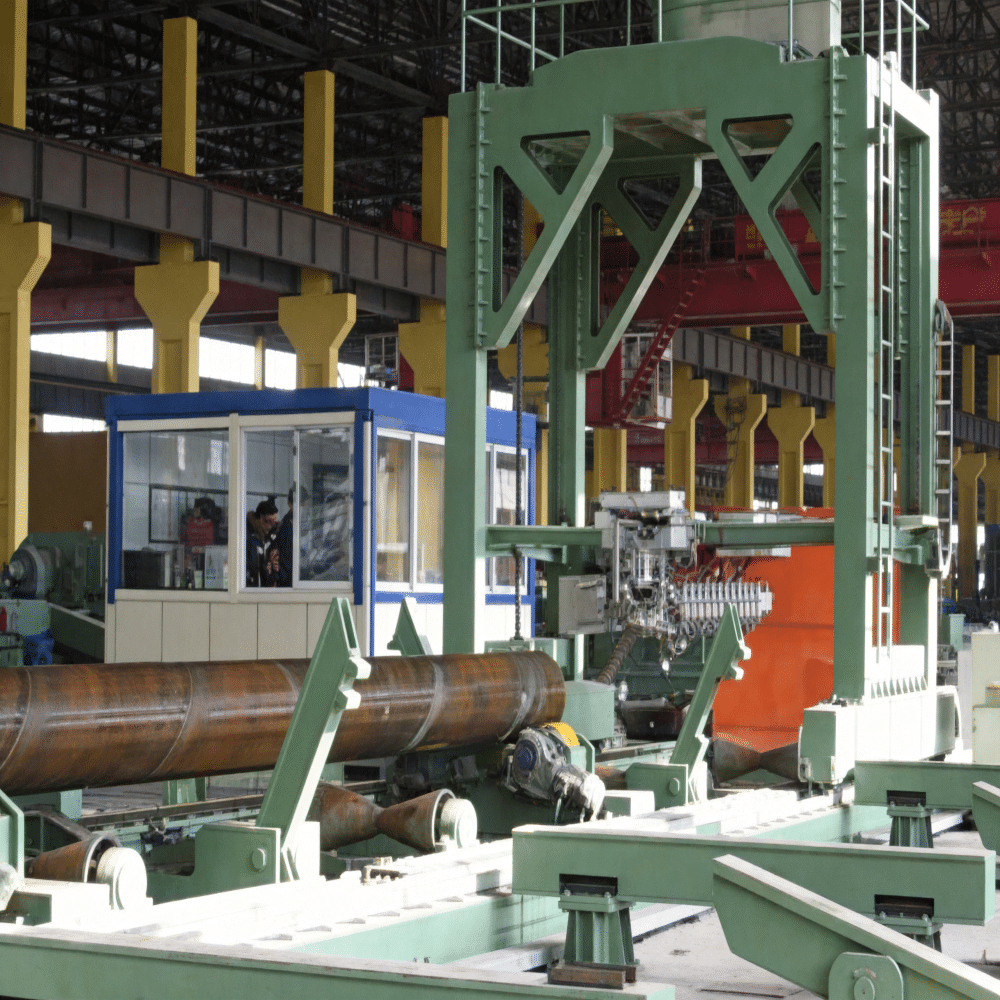
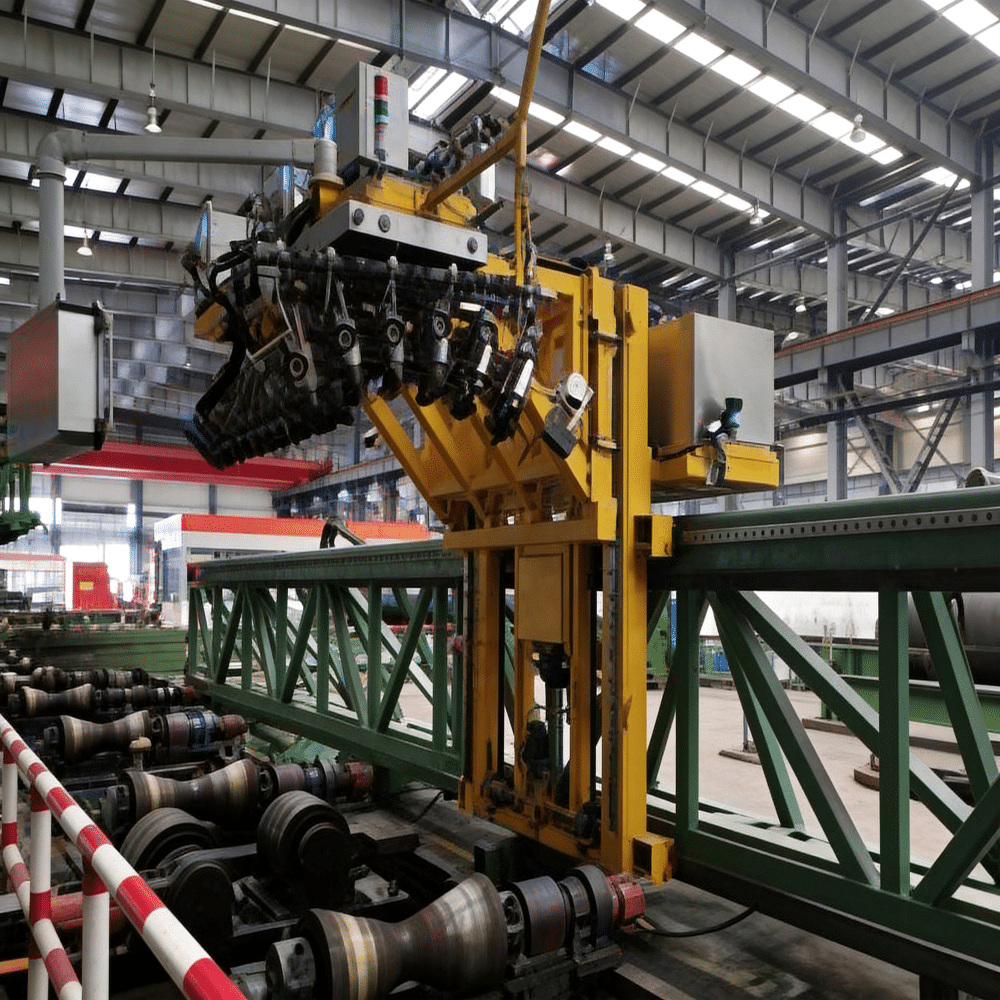
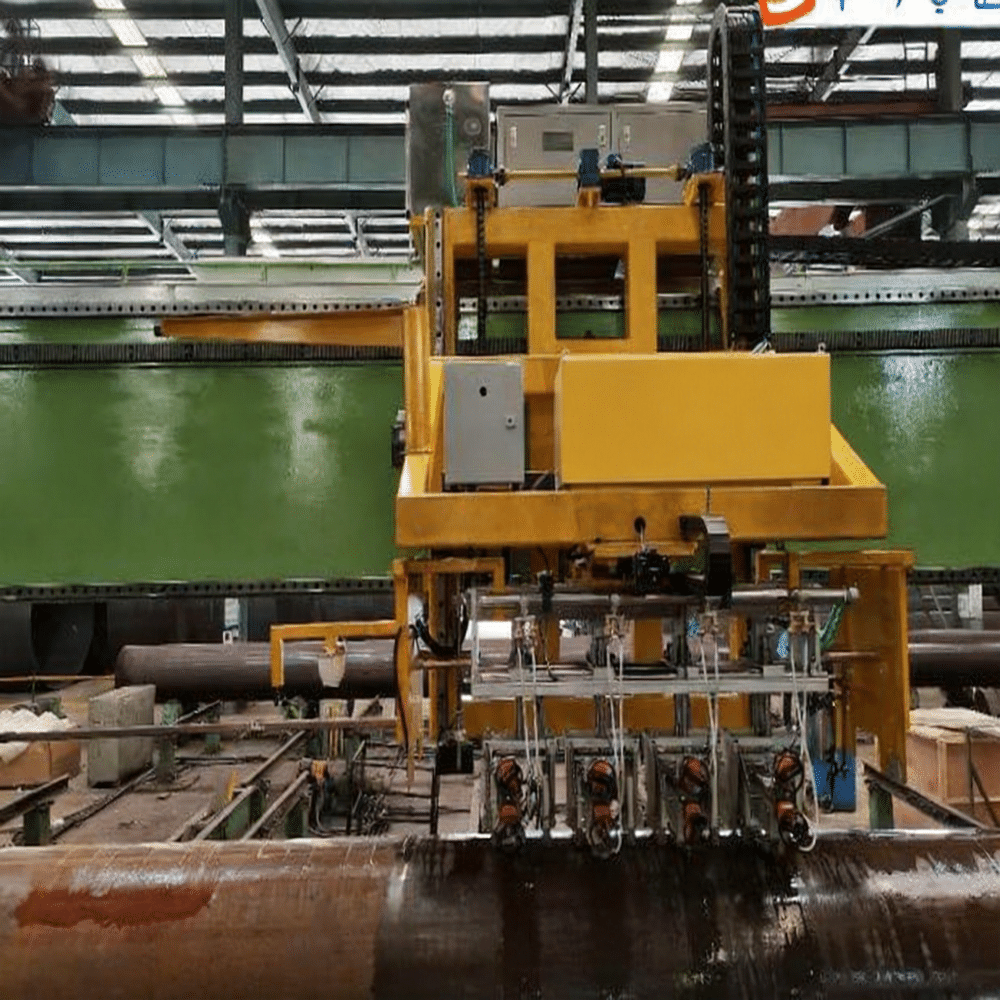
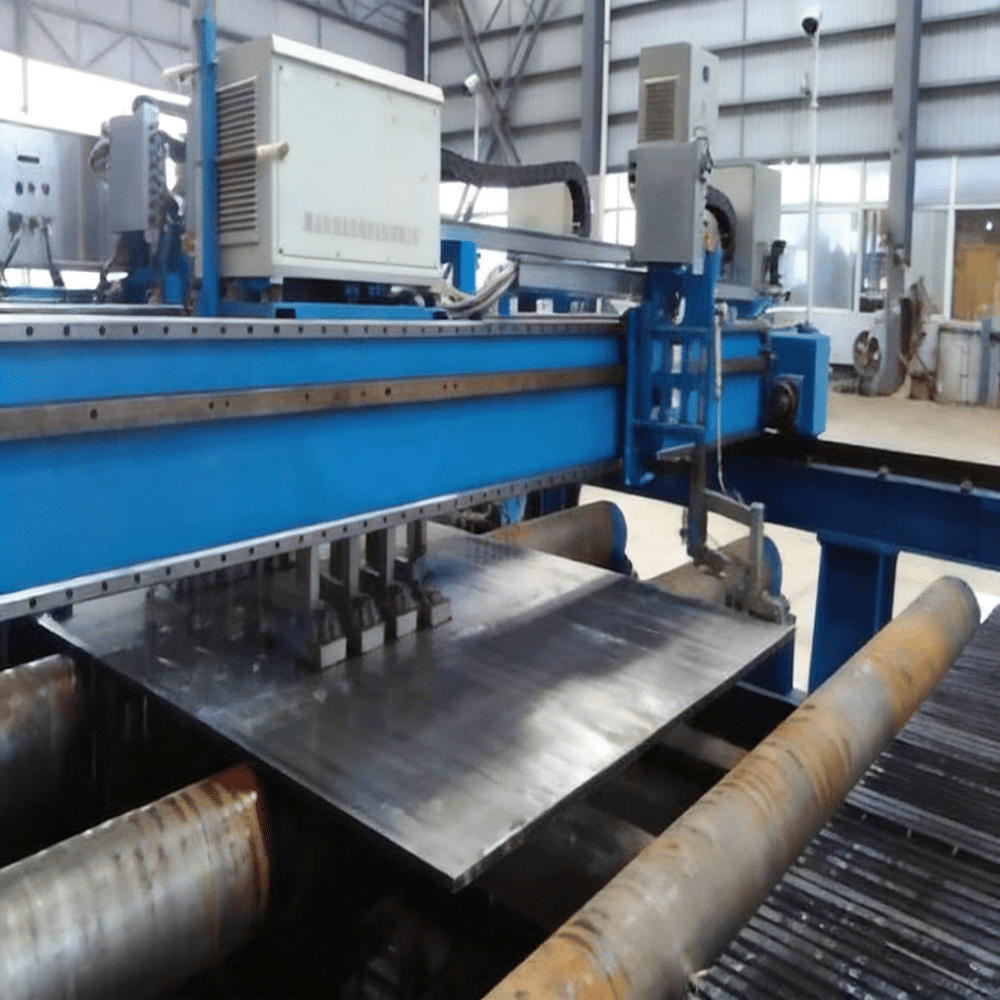
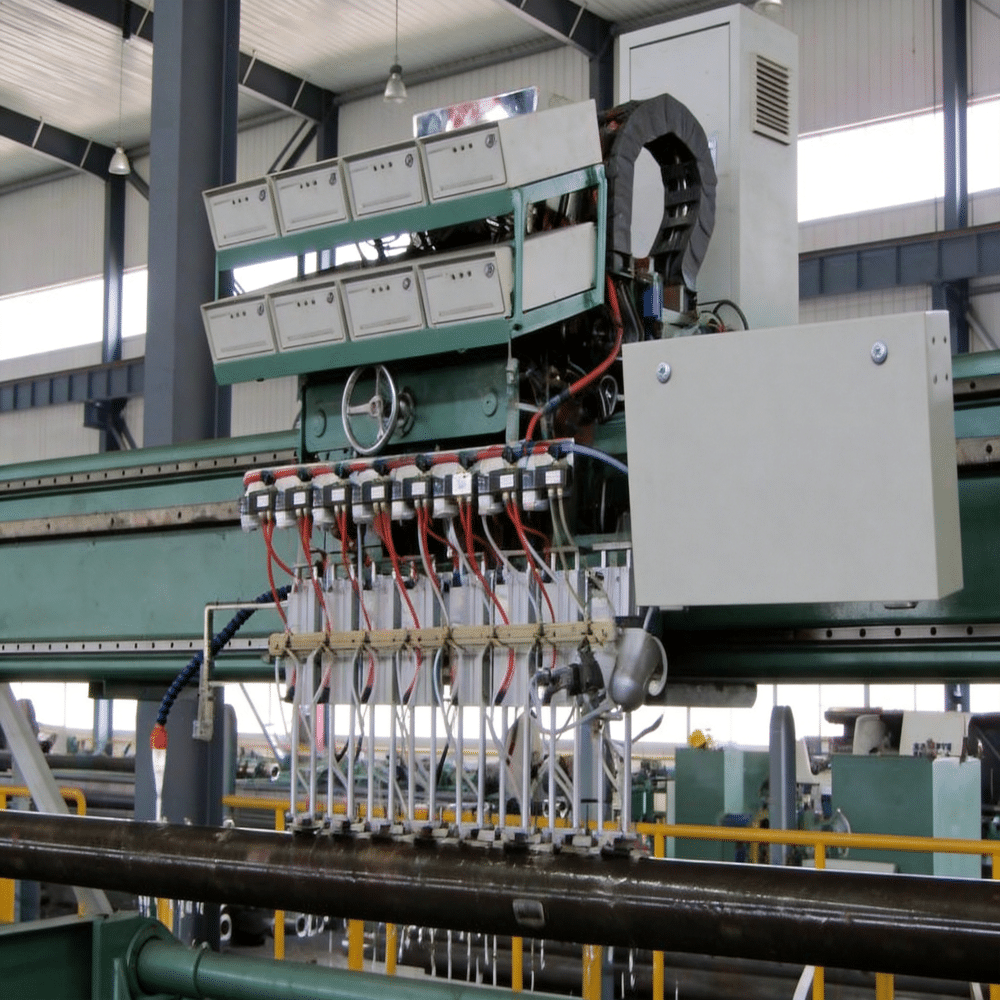
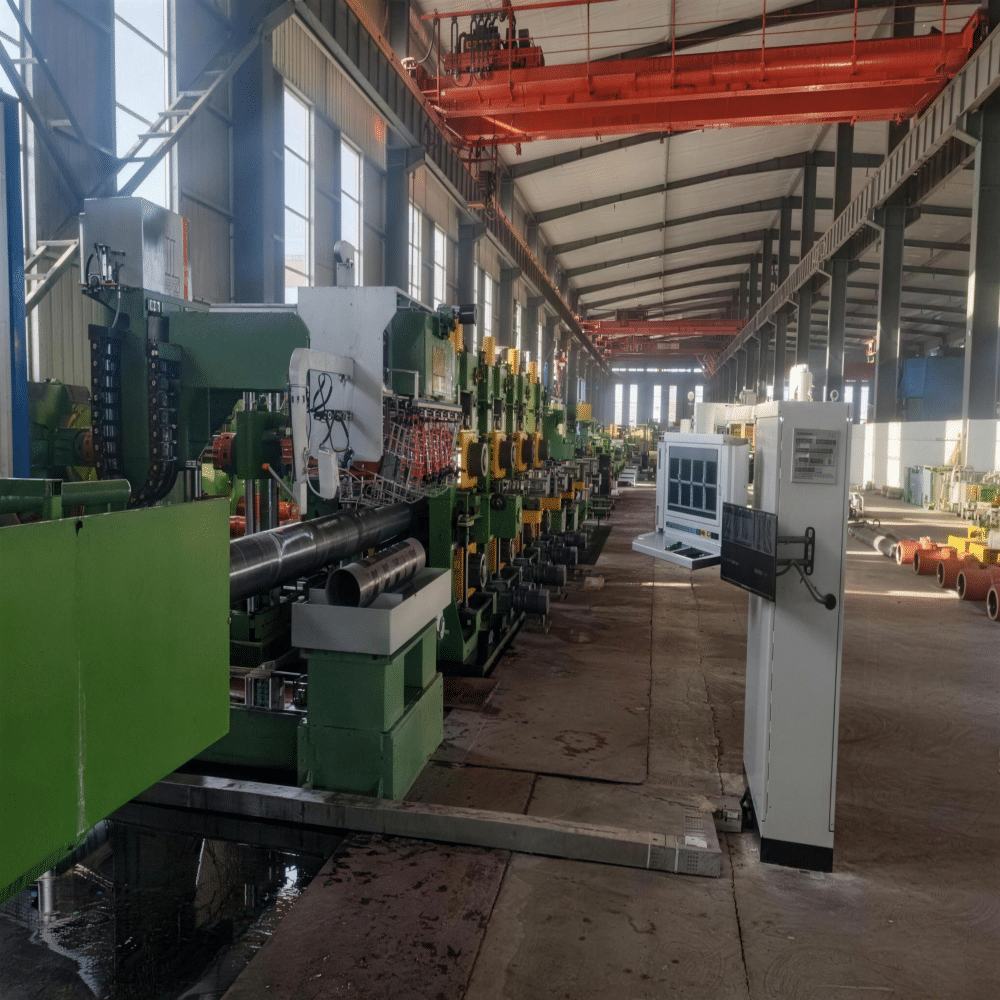
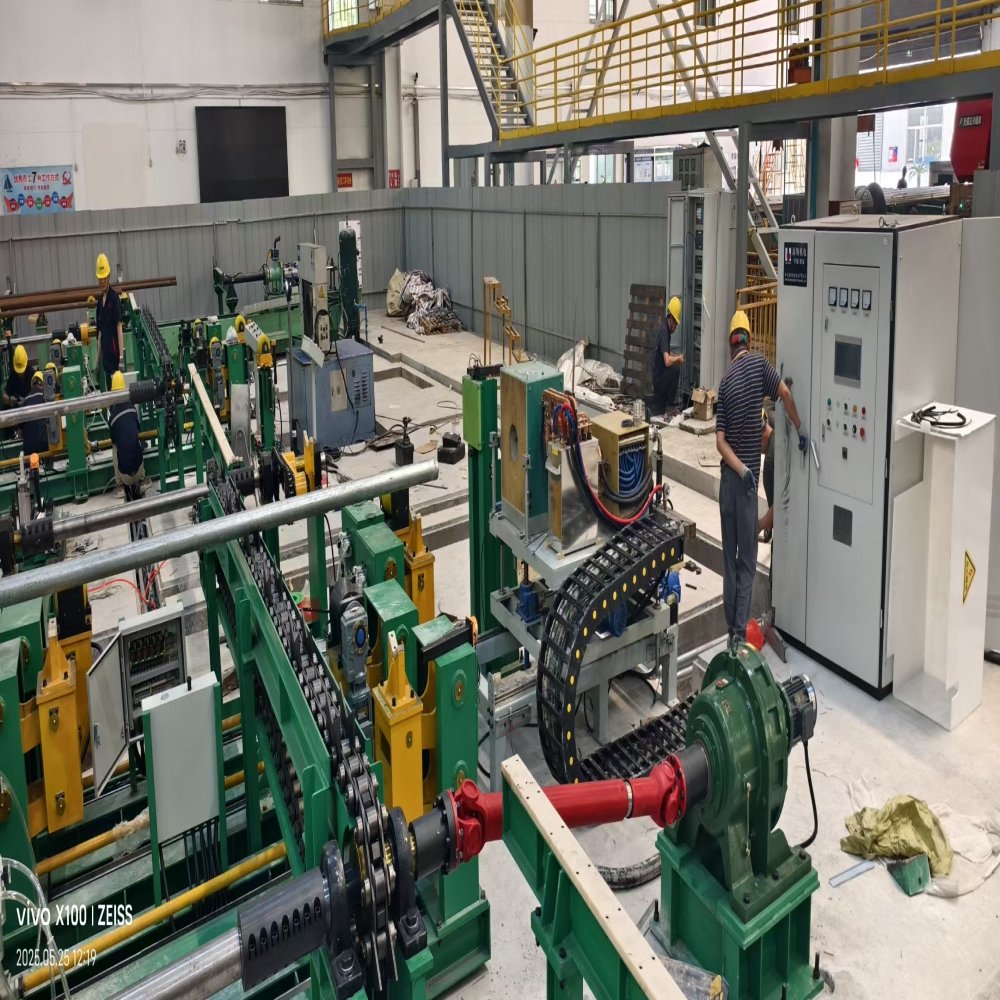
O nosso Flying Cut‑off Machine for ERW Steel Tube Line, concebido à medida para linhas de produção de tubos ERW, foi especialmente projetado para realizar o corte a frio contínuo a alta velocidade de tubos de aço de pequeno e médio diâmetro. Com uma excelente adaptabilidade, pode ser perfeitamente combinado com fresas orbitais, equipamento de corte em movimento, laminadores de tubos ERW, bem como com linhas de produção completas dedicadas a tubos de revestimento e de produção (OCTG).
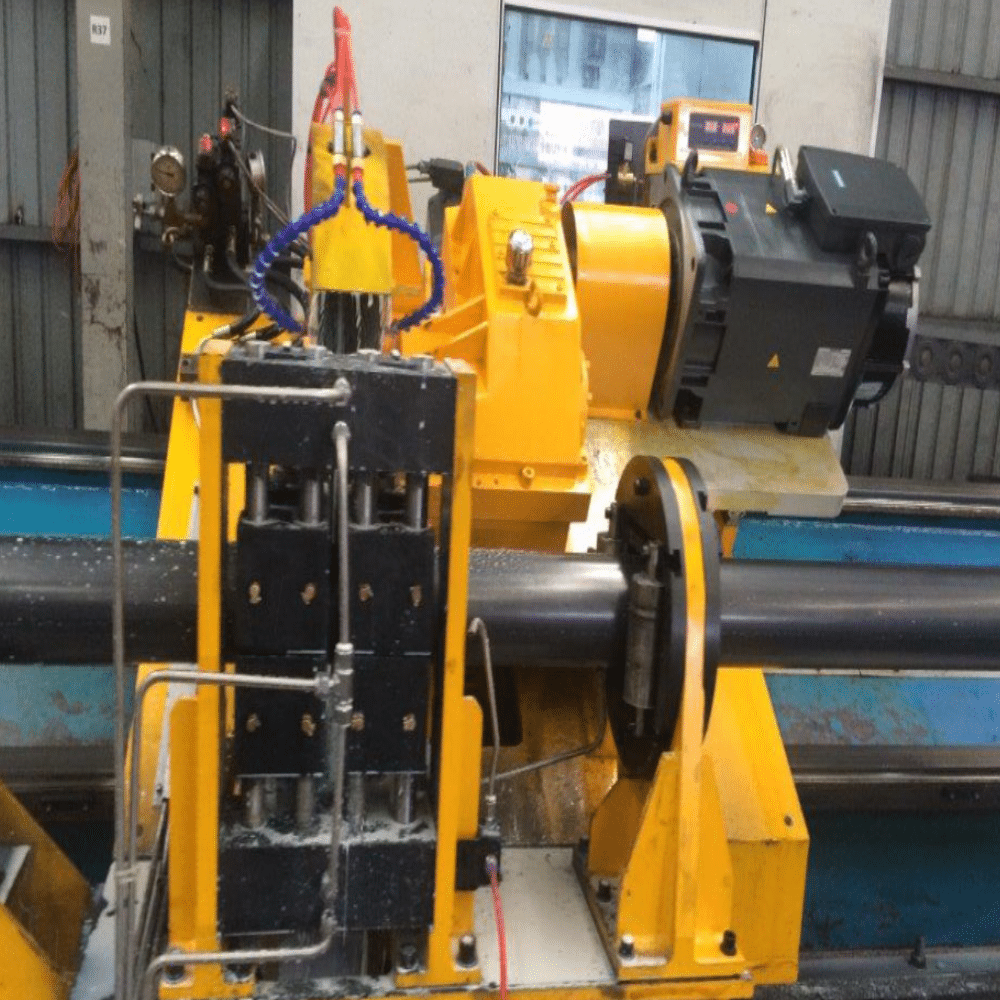
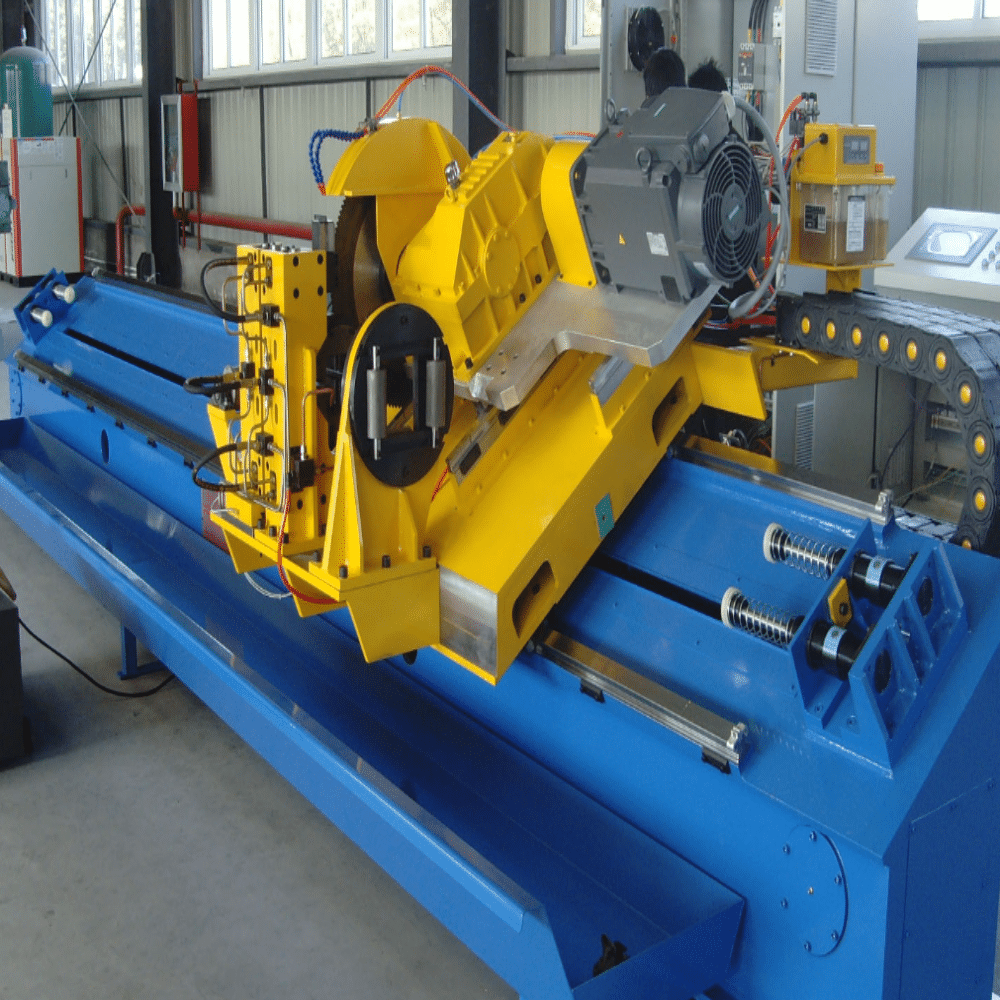
Concebida com um mecanismo de corte a frio do tipo cisalhamento e equipada com um sistema integrado de arrefecimento e lubrificação completo, a máquina dissipa a maior parte do calor gerado pelo corte através das limalhas metálicas. Este design estrutural garante que tanto as peças de tubagem como as lâminas de corte se mantenham a uma temperatura baixa ao longo de todo o processo de corte.
Capaz de funcionar a elevadas velocidades lineares, a unidade produz extremidades de tubos perfeitamente retangulares, sem rebarbas nem deformações, aliadas a uma precisão dimensional excecional. Ideal para fabricantes de tubos de elevado rendimento, este equipamento aumenta significativamente a produtividade global da linha de produção, ao mesmo tempo que garante uma qualidade de acabamento estável e superior dos tubos na produção em massa.

Especificações
| N.º do modelo. | Diâmetro do tubo (mm) | Espessura do tubo (mm) | Comprimento do corte (m) | Tolerância de corte | Velocidade da fresadora (m/min) | Quantidade de lâminas de serra | Material da lâmina de serra |
| LFJ-GH32 | Φ13-38 ◻10-30 | 0.6-2.3 | 2.0-12.0 | ≤±2 mm | Máx. 150 | 1 | TCT/HSS |
| LFJ-GH50 | Φ20-63,5 ◻15-50 | 0.8-3.0 | 2.0-12.0 | ≤±2 mm | Máx. 130 | 1 | TCT/HSS |
| LFJ-GH76 | Φ32-89 ◻25-70 | 1.2-4.0 | 2.0-12.0 | ≤±2 mm | Máx. 120 | 1 | TCT/HSS |
| LFJ-GH89 | Φ32-108 ◻30-75 | 1.5-4.0 | 2.0-12.0 | ≤±2 mm | Máx. 110 | 1 | TCT/HSS |
| LFJ-GH114 | Φ63-114 ◻50-90 | 1.2-5.0 | 3.0-12.0 | ≤±2 mm | Máx. 85 | 1 | TCT/HSS |
| LXFJ-GH114 | Φ76-127 ◻60-100 | 2.0-5.0 | 4.0-12.0 | ≤±2 mm | Máx. 85 | 2 | TCT/HSS |
| LFJ-GH127 | Φ60-140 ◻50-110 | 1.2-6.0 | 3.0-12.0 | ≤±2 mm | Máx. 70 | 1 | TCT/HSS |
| LXFJ-GH140 | Φ89-140 ◻70-120 | 2.5-6.0 | 4.0-12.0 | ≤±2 mm | Máx. 80 | 2 | TCT/HSS |
| LFJ-GH165 | Φ76-168 ◻60-130 | 2.0-8.0 | 3.0-12.0 | ≤±2 mm | Máx. 65 | 1 | TCT/HSS |
| LXFJ-GH165 | Φ114-165 ◻80-130 | 2.5-8.0 | 4.0-12.0 | ≤±2 mm | Máx. 75 | 2 | TCT/HSS |
| XFJ-GH165 | Φ48-165 ◻50-150 | 4.0-10.0 | 6.0-12.0 | ≤±2 mm | Máx. 40 | 2 | TCT |
| LXFJ-GH219 | Φ114-219 ◻100-150 | 4.0-12.0 | 2.5-8.0 | ≤±2 mm | Máx. 70 | 2 | TCT |
| XFJ-GH219 | Φ114-219 ◻60-200 | 3.5-12.0 | 6.0-18.0 | ≤±2 mm | Máx. 40 | 2 | TCT |
| XFJ-GH273 | Φ165-273 ◻60-220 | 4.0-12.0 | 6.0-18.0 | ≤±2 mm | Máx. 38 | 2 | TCT |
| XFJ-GH325 | Φ165-325 ◻80-250 | 5.0-14.0 | 6.0-18.0 | ≤±2 mm | Máx. 35 | 2 | TCT |
| XFJ-GH406 | Φ219-406 ◻80-300 | 6.0-16.0 | 6.0-24.0 | ≤±2 mm | Máx. 35 | 2 | TCT |
| XFJ-GH508 | Φ219-508 ◻100-400 | 6.0-18.0 | 6.0-24.0 | ≤±2 mm | Máx. 30 | 2 | TCT |
| XFJ-GH630 | Φ219-630 ◻100-500 | 6.0-20.0 | 6.0-24.0 | ≤±2 mm | Máx. 30 | 2 | TCT |
| XFJ-GH660 | Φ325-660 ◻100-500 | 6.0-22.0 | 6.0-24.0 | ≤±2 mm | Máx. 30 | 2 | TCT |
| XFJ-GH711 | Φ325-711 ◻100-600 | 8.0-22.0 | 6.0-24.0 | ≤±2 mm | Máx. 25 | 2 | TCT |
| XFJ-GH762 | Φ325-762 ◻100-600 | 8.0-25.0 | 6.0-24.0 | ≤±2 mm | Máx. 25 | 2 | TCT |
Princípio de funcionamento
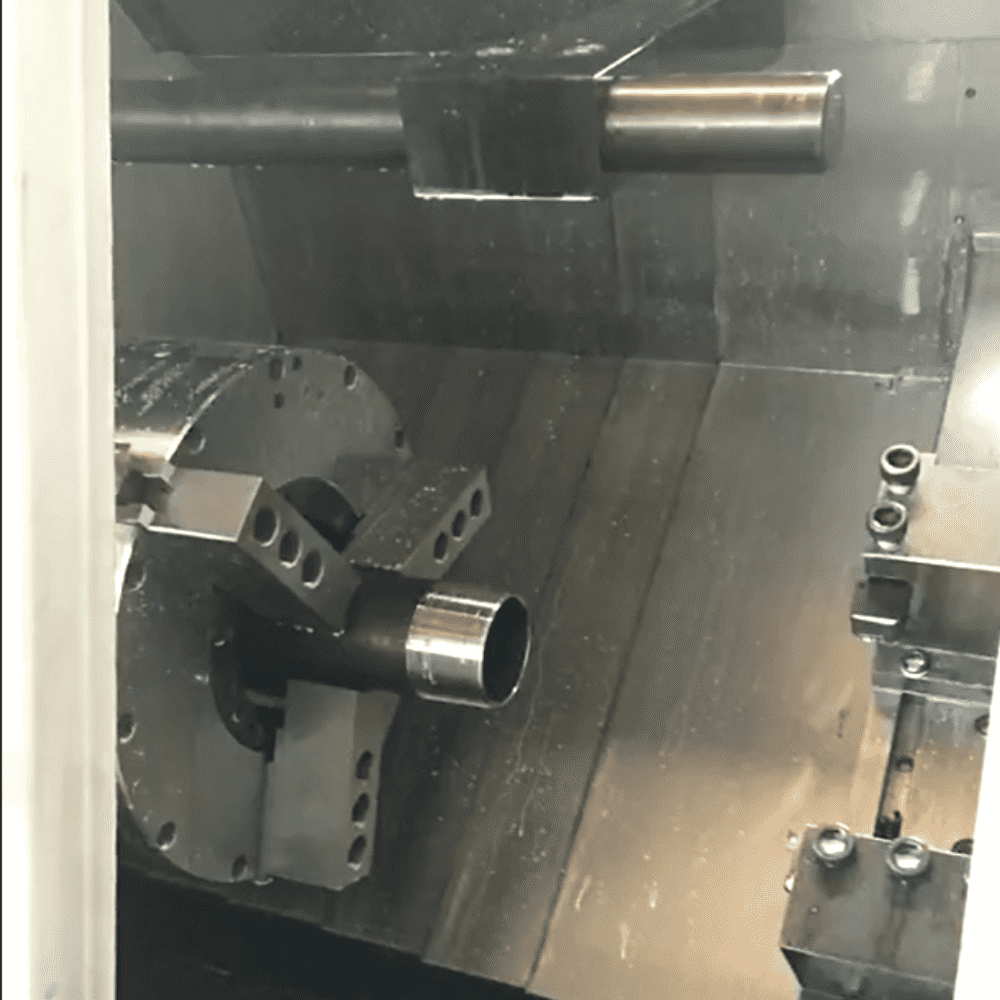
Different from traditional abrasive hot cutting discs that generate massive frictional heat and sparks, this lâmina de serra a frio simples relies on precision-ground hard cutting teeth to shear tube wall mechanically. During high-speed rotation and controlled feeding, cutting coolant continuously washes the cutting zone to dissipate heat instantly. All cutting thermal energy is taken away by swarf, so no heat-affected zone (HAZ), tube oxidation or thermal deformation occurs on pipe ends, realizing true cold cutting forming for tubular workpieces. Optimized tooth gullet design ensures smooth chip evacuation, avoiding tooth clogging during long-time high-speed tube cutting.
As nossas vantagens
- Desempenho de corte de alta velocidade para tubos de pequena e média dimensão
- Qualidade superior da superfície de corte, processamento secundário mínimo
- Longa vida útil e excelente resistência ao desgaste
- Baixa vibração e funcionamento contínuo estável
 English
 Español
 Русский
 العربية
 Français
 Português